SLS 3D Printing Quality Tips from an Advanced PA12 Powder For SLS Printing Manufacturer
Industrial Selective Laser Sintering (SLS) technology is undergoing a decisive evolution, shifting rapidly from fast aesthetic prototyping to direct digital manufacturing of functional end-use components. As industrial enterprises integrate additive systems into series production, the demand for repeatable part accuracy, zero internal defects, and consistent isotropic mechanical properties has never been higher. Achieving these strict production standards requires a deep understanding of polymer behavior during laser scanning and thermal cooling. Partnering with a reliable Advanced PA12 Powder For SLS Printing Manufacturer allows engineering teams to identify the root causes of common printing defects, adjust material parameters, and optimize powder bed interactions effectively.
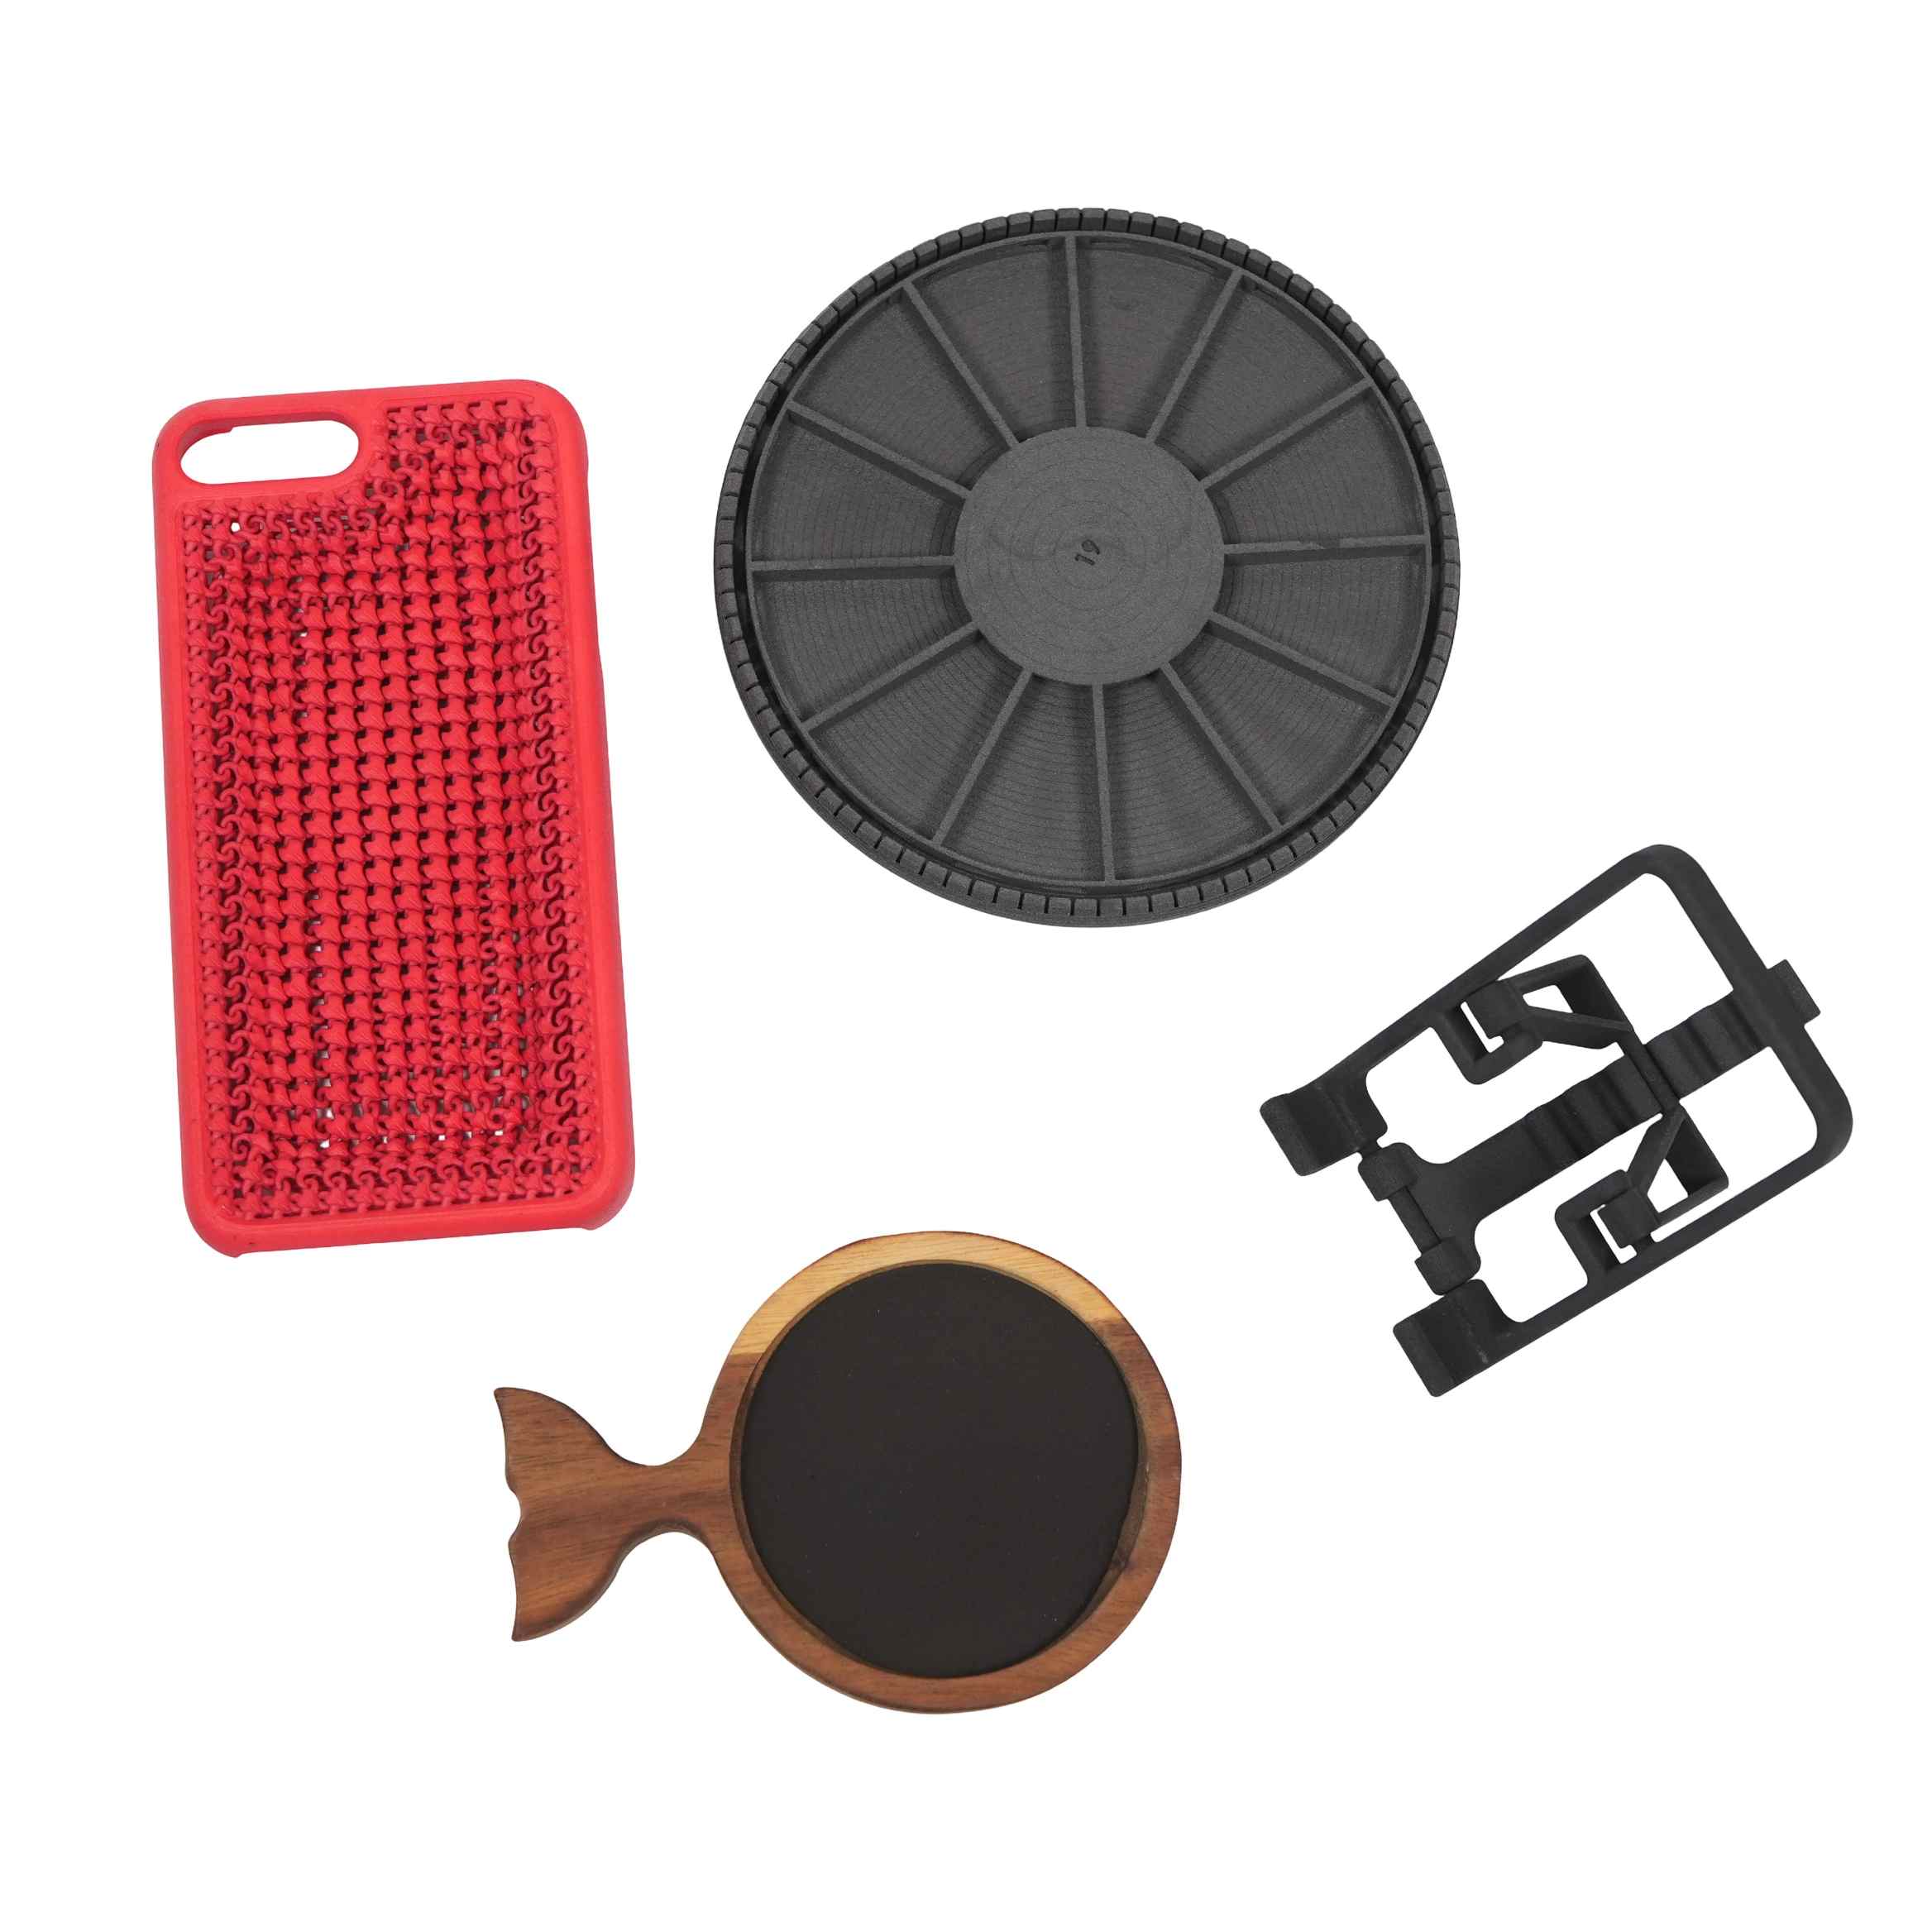
Industry Shift: Transitioning SLS from Rapid Prototyping to Low-Volume Direct Production
The transition toward Direct Digital Manufacturing fundamentally transforms how engineering teams evaluate SLS raw materials. While aesthetic prototypes tolerate minor surface roughness or slight internal voiding, functional end-use components require uncompromising mechanical integrity and tight dimensional tolerances. Consequently, manufacturing engineers must ensure that every printed layer consolidates uniformly across the entire build platform.
Material performance serves as the cornerstone of this manufacturing transition. Variations in powder particle morphology, thermal stability, or viscosity can lead to unpredictable mechanical failures under operational stress. With over 17 years of specialized expertise in polymer modification, Xiamen Bocheng Plastic Materials Co., Ltd provides technical insights that connect polymer powder chemistry directly to real-world printing performance. Understanding these underlying material dynamics helps operators solve persistent quality challenges and achieve reproducible production yields.
Diagnostic Guide 1: Eliminating Surface "Orange Peel" Through Particle Size Distribution Control
Surface roughing, commonly known as the "orange peel" effect, remains one of the most frequent defects in SLS components. This issue typically stems from uneven powder bed spreading, erratic fluidization, and localized melt agglomeration during laser scanning. When powder contains an excessive concentration of fine particles or an overly broad particle size distribution, recoater blades create drag marks across the build area.
Different polymer processing methods require specific particle size profiles to function efficiently. For example, electrostatic spraying techniques typically utilize particles with a median diameter (D50) between 35 and 45 micrometers to optimize surface charge adhesion. Conversely, fluidized bed dip coating relies on coarser particles ranging from 80 to 120 micrometers for gravity immersion. For industrial SLS additive manufacturing, optimal performance requires a strictly controlled spherical distribution where D50 ranges from 45 to 50 micrometers, D10 remains between 25 and 30 micrometers, and D90 stays within 70 to 75 micrometers. Maintaining a tight particle size distribution span—calculated as Span = (D90 - D10) / D50—below 1.0 prevents powder segregation.
To address this technical hurdle across specialized 3D printing applications, BOCHENG employs sub-zero cryogenic milling at minus 100 degrees Celsius followed by precision multi-stage air classification. This process yields the BC-PA12-S01 grade, which features a uniform bulk density between 0.45 and 0.50 grams per cubic centimeter and a low angle of repose at 32 degrees. These physical properties ensure smooth fluidization, consistent layer deposition, and smooth surface finishes free of orange peel defects.
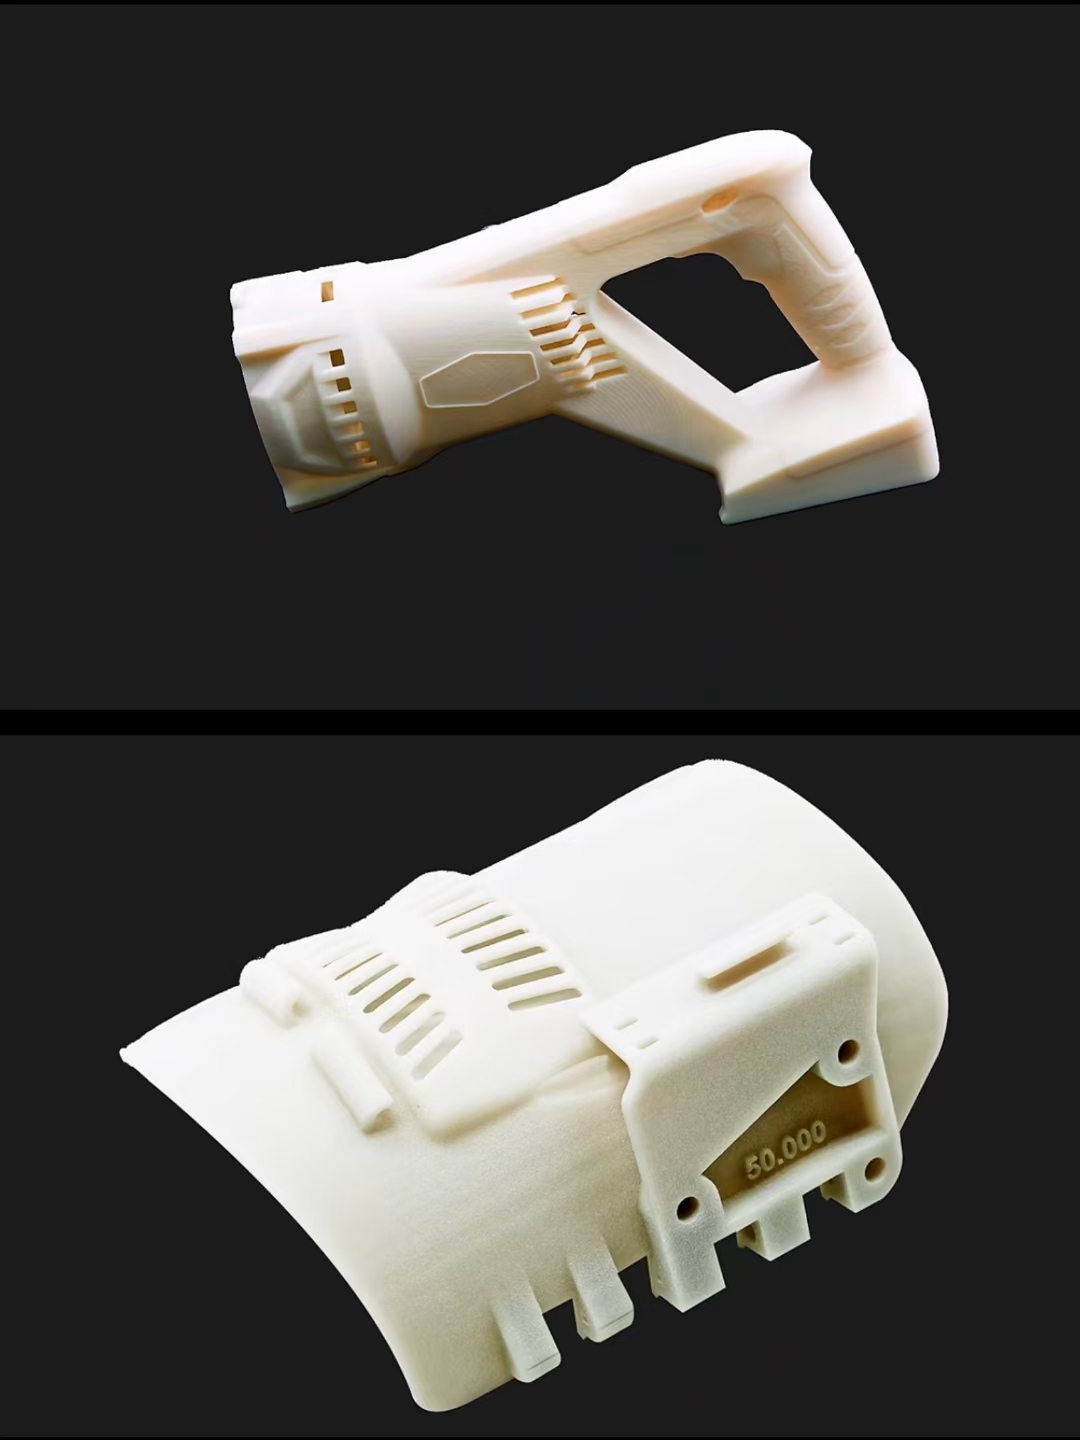
Diagnostic Guide 2: Solving Internal Porosity via Optimized Powder Refresh & Viscosity Management
Internal porosity severely compromises the tensile strength, impact resistance, and fluid tightness of printed parts. Microscopic voids inside the component usually develop when the molten polymer exhibits high melt viscosity, which prevents complete particle coalescence before solidification occurs. This elevated viscosity frequently results from thermal aging when virgin powder mixes with recycled material that has undergone multiple heating cycles.
During extended printing runs, polyamide powders experience post-condensation reactions in the build chamber. This thermal exposure increases molecular weight and lowers the Melt Flow Rate (MFR). Consequently, heavily aged powders fail to flow together smoothly when struck by the laser beam, trapping air pockets between powder granules. Managing the refresh ratio—the proportion of virgin powder added to used powder—is crucial for maintaining consistent rheological properties.
To eliminate internal voiding, BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) formulates its PA12 materials with proprietary heat-stabilizing additives that broaden the sintering window to 20–30 degrees Celsius. Featuring a precise melting point of 181 degrees Celsius and a crystallization temperature between 145 and 155 degrees Celsius, the material resists thermal degradation during prolonged build cycles. As a result, operators can maintain a flexible refresh ratio between 30% and 70% while keeping internal part porosity under 1%, preserving both structural integrity and operational cost efficiency.
Diagnostic Guide 3: Overcoming Poor Interlayer Adhesion & Warpage via Thermal History Control
Interlayer delamination and part curling present significant obstacles to achieving dimensional accuracy and isotropic strength. These defects occur primarily when build chamber temperature gradients fluctuate outside the strict sintering window. If the bed temperature drops below the crystallization threshold—typically kept between 165 and 175 degrees Celsius—the polymer crystallizes prematurely, creating internal contraction stress and layer warping.
Controlling the thermal history of the powder bed throughout multi-hour print runs prevents uneven crystallization shrinkage. Furthermore, excess moisture in raw powders can cause hydrolytic degradation at elevated temperatures, leading to unpredictable mechanical properties and weak layer bonding. Maintaining rigorous control over environmental storage conditions and raw material specifications eliminates these variable parameters.
Engineers address these challenges by enforcing strict raw material moisture thresholds below 0.1%. Comprehensive five-stage quality control testing across every production batch guarantees predictable thermal absorption during laser scanning. This uniform thermal response minimizes inter-layer boundary weakening and delivers consistent z-axis shear strength, ensuring that complex structural components remain flat and dimensionally stable.
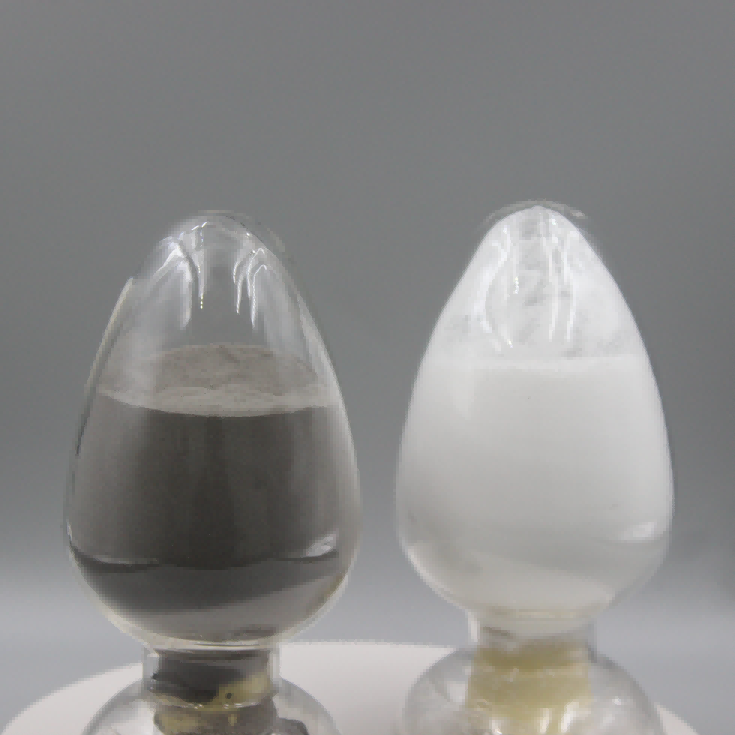
Beyond Standard PA12: Advanced SLS Portfolio & OEM Supply Capabilities
As industrial applications diversify, specialized polymer formulations are required to meet demanding mechanical and thermal specifications. Beyond standard polyamide powders, specialized composite grades expand the functional capability of additive manufacturing equipment in automotive, aerospace, and consumer goods sectors.
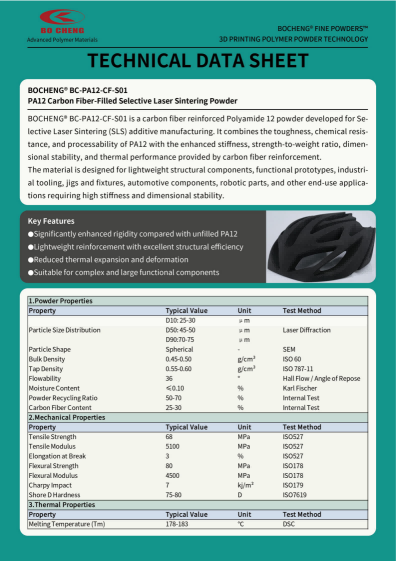
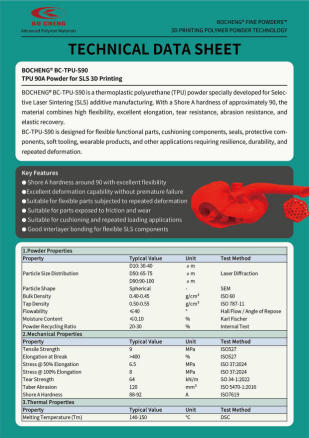
The composite portfolio includes BC-PA12-GF-S01, a glass-reinforced powder containing 20% to 25% glass spheres that achieves a Heat Deflection Temperature (HDT at 1.8 MPa) of 168 degrees Celsius for rigid structural enclosures. Additionally, BC-PA12-CF-S01 incorporates 25% to 30% carbon fibers to deliver a tensile modulus of 4500 MPa for lightweight functional parts. For applications demanding high impact resistance or flexibility, BC-PA11-S05 provides elongation at break exceeding 30%, while BC-TPU-S90 offers elastomeric performance rated at Shore 90A.
To support global industrial supply chains, products are packaged in 25-kilogram heavy-duty moisture-proof sealed containers to ensure long shelf life during transit. Customized powder color options and material property modifications are also available to meet specific OEM manufacturing requirements. BOCHENG supports international clients with efficient delivery turnaround times of 7 to 15 days, supported by flexible global trade settlement channels including T/T and VTB Bank options. Operating under ISO 9001 and IATF 16949 quality management certifications, alongside USP Class VI biocompatibility compliance, the enterprise continues to advance polymer materials for global additive manufacturing applications.
For more technical documentation and product details, visit the official website: https://www.pa6-pa66.com/.